How to Integrate Overhead Cranes into Automated Production Lines
The position of manual bridge cranes in most production lines is a bit awkward.The operator occupies the post, and the hoisting action of the bridge crane is limited by the reaction speed of the person, the beat is unstable, and the waiting time for loading and unloading is long. It will also cause a backlog of WIP due to the irregular lifting trajectory of the bridge crane.These seemingly daily small problems, once the beat of the production line accelerates, will become bottlenecks.The purpose of connecting the bridge crane to the automated production line is not to replace a more expensive equipment, but to let the bridge crane and the entire line run at the beat.An automated hoisting line with stable operation can usually compress the single cycle time by 20% to 40%, and reduce the labor consumption of loading and unloading to close to zero.
How Do Overhead Cranes Work in Automated Production Lines?
Crane automation Basics
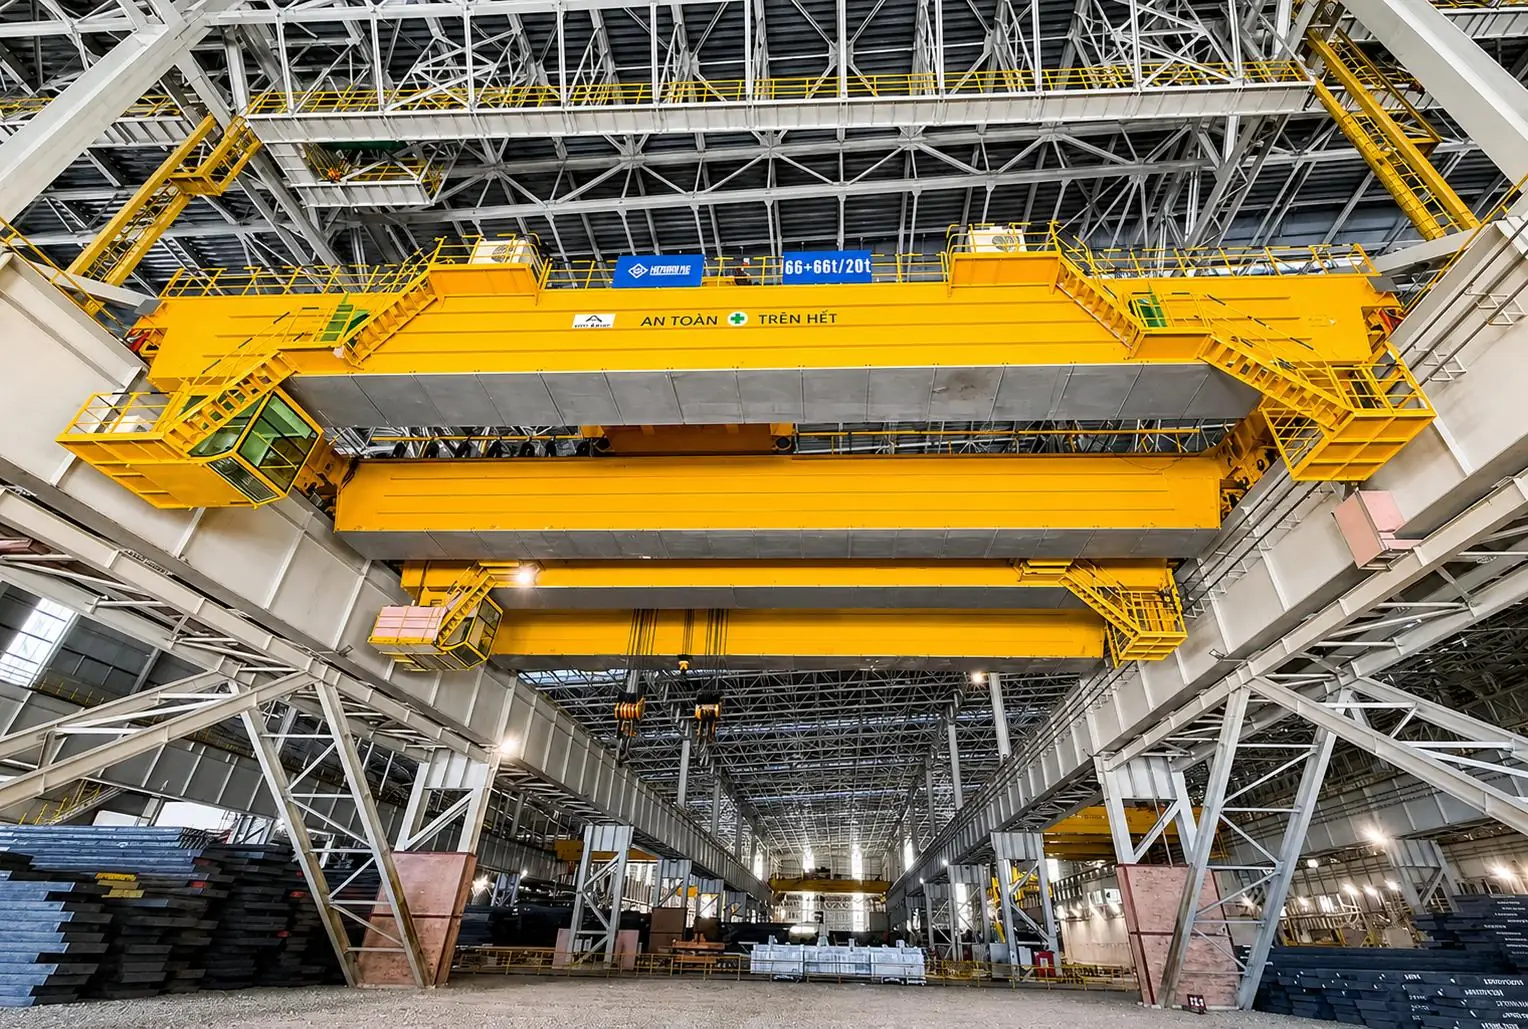
The automation of Henan Mine Crane Factory supply bridge cranes is not just to replace operators with robots, but to upgrade the three sets of mechanisms of carts, trolleys and hoisting, so that the operation of each mechanism can be executed in accordance with preset procedures, combined with the positioning and dispatching system, to realize the automatic operation and collaborative operation of bridge cranes, and gradually transform manual operation into system control.The degree of automation is usually divided into three levels.The first level is remote control. The operator uses a handle or tablet to control in a safe area to reduce personnel risks without changing the operating mode.The second level is the execution of the scheduled procedure. The bridge crane automatically completes the handling according to the set path and action, and the person is only responsible for triggering it.The third level is fully automatic scheduling linked to the beat of the production line. The bridge crane receives tasks directly from the system and completes the whole process of picking, transporting and discharging independently.Which level of production line to choose depends on the status of existing equipment and acceptable transformation investment, not on the old and new equipment.The old bridge crane can also enter the second or even third level through electrical and control upgrades.
System integration
Integration means turning the bridge crane into part of the production line, not just a usable hoisting tool.The typical practice is to let the upper system uniformly issue tasks, and the bridge crane only performs three actions: picking, transporting, and releasing.After the task instruction arrives, the system plans the path, and the bridge crane reclaims the material, transports it in place, and returns without load to form a complete closed loop.The actual benefit of integration is the synchronization of material flow and information flow.In the past, when the materials were in place depended on manual scheduling, but now they are uniformly arranged by the system. The backlog of WIP has been significantly reduced, and the waiting time at the bottleneck station has been compressed.This part of the benefit is not achieved by speeding up the speed of the bridge crane, but by eliminating the scheduling wait.This is also the most real source of value for automation transformation.
Automation technology
Supporting the landing of automation are several key technologies.The frequency converter of the bridge crane is combined with a closed-loop encoder to make the three-axis movement speed controllable and the position repeatable.Laser ranging or QR code positioning provides the absolute position reference of the bridge crane.The anti-swing algorithm suppresses the swing of the bridge crane crane in operation and ensures the accuracy of placement.Safety laser scanners and gratings delineate the work area and isolate personnel from the danger zone.Each technology solves a specific problem.When selecting the type, first look at the requirements of the production line for positioning accuracy and beat. The higher the accuracy requirements, the higher the sensor level, and the cost and implementation difficulty will increase accordingly.However, one thing cannot be saved. Anti-swing and safety protection devices are required, not optional, in any bridge crane automation solution.
How to Integrate an Overhead Crane into an Existing Production Line
Workflow evaluation
Do a beat analysis before the transformation of the bridge crane, and this step determines the direction of the transformation plan of the bridge crane.Count the loading and unloading time, waiting time, and invalid walking distance of each lifting of the bridge crane, find the bottleneck station, and then see where automation can save time.Without this foundation, no matter how beautifully the plan is made, it is empty.Transformation goals must be quantified.Clarify the target cycle time, target throughput, and target manpower savings, and write the plan as the basis for acceptance, otherwise it is impossible to judge whether the project meets the standards after completion.At the same time, check the existing interface of the production line, the in-place signal of the conveyor line, the alignment point of the station, and the physical state of the bridge crane track, which determine the workload and cost range of the transformation.
Crane selection
The selection of bridge cranes revolves around a set of core parameters, such as rated lifting weight, span, lifting height, operating speed, working level and expected frequency of use.Each item directly affects the boundary of the production capacity of the bridge crane after the transformation. It cannot be allocated only according to the current minimum demand, and there must be room for climbing.Three things are reserved for the automation of bridge cranes, sufficient walking and lifting speed margin, communicable frequency conversion and PLC interface, and the hardware foundation for positioning and anti-swing functions.Many projects wanted to upgrade in the later stage, but found that the bridge crane did not reserve the interface at the beginning, and was forced to replace the whole machine, doubling the cost.Taking these points into account when selecting the model can save a large amount of subsequent renovation costs.
PLC and control integration
The controller of the bridge crane must be docked with the production line PLC, and the communication method of the bridge crane control system must be determined first.The common Profinet, ETHERNET/IP, and Profibus fieldbuses have their own applicable scenarios. The selection depends on the existing PLC brand and network architecture of the production line. It is best to be consistent with the production line and reduce the protocol conversion link.The interaction logic of bridge cranes should be clearly defined.The PLC of the production line sends signals for placement, pick-and-place, and release, and the bridge crane is executed in the order of the signals. The two ends are interlocked and mutually recognized, and neither end is ready to operate.Redundancy design must also be done in the control, master-slave communication, manual and automatic switching, and fault downgrading.When automation fails, the operator can switch back to manual takeover at any time without interrupting production.
Conveyor coordination
The cooperation between the bridge crane and the conveyor line depends on the alignment logic.The three elements of in-place detection, load identification, and release confirmation form an interlocking. The bridge crane will only release the material if it confirms that the station is ready, and the conveyor line will only continue to feed if it confirms that the spreader has left. There will be no empty runs on both sides, and there will be no crashes.In multi-station scenarios, the scheduling priority must also be defined.The bridge crane can only serve one station at a time. The system should prioritize the urgency of the task and the status of the station to avoid path conflicts when multiple tasks are concurrent.This step is done carefully, so that the collaborative efficiency of the bridge crane and the conveyor line can be guaranteed.
Sensor integration
Automation relies on sensors much more than manual operation.The load of the bridge crane is weighed to determine whether it is overloaded and correctly grasped. The position detection covers the dual axles of walking and lifting, anti-collision ranging to avoid collisions, and alignment confirmation to ensure the discharge accuracy of the bridge crane. , Safety protection keeps people away from the work area.These types of sensors form a complete perception layer.Key signals must be redundant and self-checked.The important sensor adopts a dual-channel design, coupled with a fault self-test, to ensure that a single sensor can trigger a safe shutdown when it fails, rather than malfunction.The sensor calibration and calibration of bridge cranes also directly affect the positioning accuracy and cycle time, and should be included in the daily maintenance plan.
What Challenges Affect Crane Automation Projects?
Building and runway restrictions
Plant conditions are often the biggest variable in bridge crane automation projects.The headroom height determines the lifting and spreader transformation space, the straightness and wear of the track directly affect the positioning accuracy of the bridge crane, and the foundation bearing and column spacing constrain the span and load.Do a check of the status quo of the bridge crane plant before the transformation, which can avoid rework where the equipment is in place and the track is found to be unqualified.The difference in construction investment between the new factory building and the renovation of the old factory building is obvious.We can take into account the track accuracy and automation interface at the design stage.For the old plant, it is necessary to evaluate whether the existing structure can carry the accuracy requirements of automated operation, and this part of the investment must be included in the total budget in advance.
System compatibility
Compatibility with old equipment is the most common obstacle to the transformation of bridge cranes.The electrical system of the bridge crane that left the factory in the early years was aging, incompatible with the new bus and the upper system, and direct docking often failed.At this time, it is necessary to judge which way to go, the whole machine control cabinet is transformed, or the whole machine is replaced.The judgment is based on the remaining equipment life, mechanical status and control upgrade space of the bridge crane.The mechanical condition is good, but the electrical aging is only good, and the transformation of the control cabinet is cost-effective.The equipment itself has reached the end of its life, but the transformation is not cost-effective, and the whole machine should be replaced.Do a communication protocol and I/O point check before the transformation, and use a written interface list to lock the compatibility range to avoid wrangling in the middle of the project.
Production downtime
The risk of shutdown is one of the most worried issues for the owners of bridge crane renovation projects.The commissioning, trial operation and acceptance of bridge cranes during the transformation period all require a shutdown window, which directly conflicts with the tasks in production.If it is not handled well, a transformation may interrupt several weeks of continuous production.The countermeasure is to be implemented in stages.First debug the stand-alone machine and adjust the movement of the bridge crane itself.You are welcome to join us.The final cut is fully automatic to verify the beat and stability.Every step is completed in the window to minimize the impact of the shutdown.Continuous production lines can also use night or weekend windows, or arrange the transition of alternate work plans.
Safe and reliable
The automation system of Henan Mine Crane Factory supply bridge cranes must meet safety standards and risk assessment requirements.There is no shortage of safety devices such as limit, anti-collision, emergency stop, and area protection, and the requirements for bridge crane automation scenarios are more stringent.The system has no human adaptability, and safety redundancy directly determines the risk level of the bridge crane.The reliability requirements are also higher than manual operation.During automated operation, a fault location error may cause the entire line to shut down.Therefore, fault diagnosis, redundancy design and maintainability must be considered in advance.The operating rate is the real result of the automated transformation of bridge cranes, not just the ability to run automatically.
How to Plan Crane Automation Costs and Implementation
Project cost factors
The cost of bridge crane automation transformation is not a fixed number, it depends on the scope of bridge crane transformation, the status of equipment and the complexity of the production line.The cost structure usually includes hardware (frequency converter, sensor, control cabinet), software (scheduling logic and upper system), engineering design, on-site commissioning, and personnel training.The cost level is most affected by two factors, one is the scope of transformation, whether it is the transformation of the whole machine or the addition of automation modules.The second is the electrical condition of the existing bridge crane.When estimating, it is recommended to quote separately according to the four pieces of hardware, engineering, commissioning, and training, and then superimpose the emergency budget.The ROI should be calculated in the general ledger, adding up the three items of labor savings, production capacity improvement, and waste loss reduction, and generally seeing a return of one to three years, depending on the production line utilization rate of the bridge crane.
Installation and commissioning
The implementation cycle of the bridge crane is divided into five stages, including plan design, factory commissioning, on-site installation, online trial operation, and formal acceptance.Each stage must have a clear acceptance node for bridge cranes, rather than waiting for all of them to be completed before seeing the results.Factory debugging is easy to be underestimated, but the value is very high.Simulate the on-site working conditions of the bridge crane in the factory, and adjust the action, positioning accuracy, and safety interlocking of the bridge crane itself in place, which can greatly compress the on-site commissioning time and shutdown window.After the site is connected, it will be accepted one by one according to the positioning accuracy, cycle time, and safety interlock function, and all of them will be put into operation only if they meet the standards. Do not run with illness.
Long-term maintenance
The maintenance of automation equipment is different from that of traditional bridge cranes.The sensors and encoders of bridge cranes need to be calibrated regularly, the control cabinet should pay attention to heat dissipation, and the communication stability should be inspected.These tasks may seem trivial, but they are essential for the long-term stable operation of bridge cranes.Predictive maintenance is the direction.Monitor temperature, vibration, motor current and other parameters through operating data, give early warning before a failure occurs, and turn unplanned downtime into planned maintenance.The supply of spare parts and service response of bridge cranes should also be discussed clearly when purchasing.The long-term cost of ownership should be included in the total cost, rather than just staring at the purchase price.
How to Choose an Overhead Crane Manufacturer for Automation Projects
Engineering ability
When choosing a bridge crane manufacturer, it depends not only on the product model of the bridge crane, but on the program ability.Almost all bridge crane automation projects have customized requirements. Whether non-standard design and feasibility simulation can be done for specific working conditions is more important than whether there are ready-made products.The method of investigation is to see if the other party has an engineering design team that integrates mechanical, electrical, and software, rather than just doing mechanical matching.Verify the opponent's level with specific working conditions.Throw out a scene of a large-span, heavy-duty or high-speed bridge crane, and see the depth of the plan given by the other party, whether it applies the standard plan, or is really designed around your production line, you can judge in a few words.
Control system integration
The control ability is the core of the bridge crane automation project, and it is also where the supplier gap is opened.Investigate whether the other party has independently mastered the PLC and drive programming of the bridge crane, rather than just purchasing a third-party control box to install it.Autonomous control means that subsequent changes to procedures, functions, and troubleshooting are all in your own hands, and you are not subject to others.Openness is also critical.For bridge crane control to be able to interface with MES and third-party PLCs in the production line, suppliers should keep the agreement open, rather than binding their own private agreements.The risk of binding the agreement is that any changes in the later stage must pass through the supplier, and the cost and time are uncontrollable.You can ask the other party to provide automation integration cases of bridge cranes in the same industry to verify their true integration capabilities.
Testing and technical support
Factory test data is hard evidence to judge the strength of suppliers.The full-load, full-speed, and precisely positioned bridge crane test report can visually reflect the true performance of bridge crane equipment, rather than relying only on the promotional parameters on the product information.Suppliers are required to provide complete test records as the basis for acceptance.After-sales service is the basis for long-term cooperation.The response speed of on-site commissioning, the ability of remote support, the degree of localization of spare parts, and the terms of the maintenance agreement determine the level of guarantee after the bridge crane equipment is put into operation.Once the bridge crane is shut down, it affects the entire production line. After-sales responsiveness is more important than the purchase price. Be sure to write the service level clearly in the contract.
Henan Mine Crane Factory Custom
Henan Mining Factory provides customized bridge cranes, gantry cranes and material handling solutions for demanding industrial applications. From upgrading capabilities and span to working conditions, operating mechanisms and automation requirements, each project can be customized according to specific production needs. With integrated R&D, engineering design, manufacturing and service capabilities, we help customers choose lifting equipment that is suitable for their facility layout, material handling work flow and long-term operational goals.
Whether you are upgrading an existing workshop, expanding a production line, or planning a new industrial facility, our team can work with you to define the correct crane configuration for your project. Share your required lifting capacity, span, lifting height, working environment and operating requirements, discuss customized solutions with Henan Mining Cranes, and plan your project from planning to implementation